
Direct Manufacturer of High-Tech Architectural Coatings
-
30,000m² Facility: 15 automated lines for stable B2B production.
-
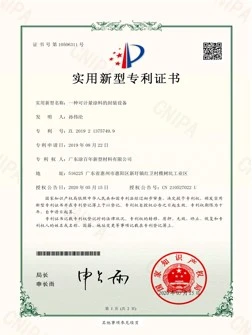
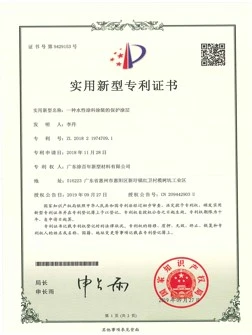
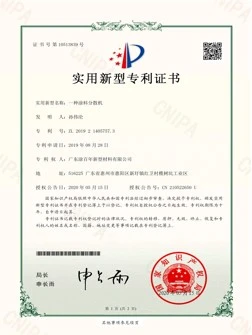
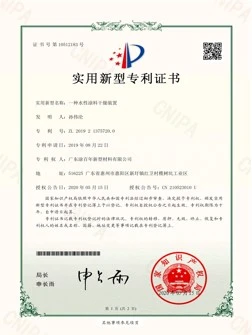
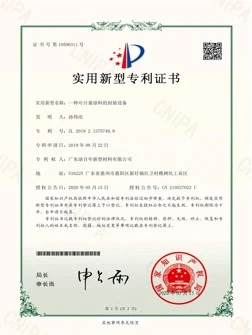
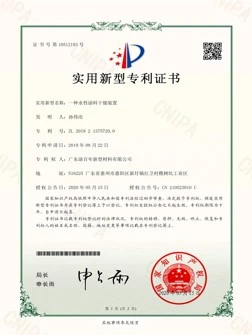
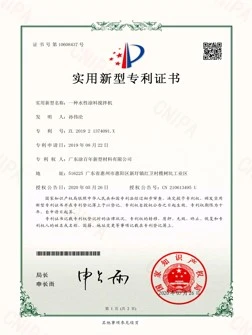
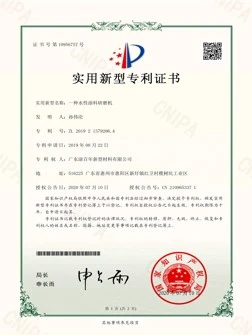
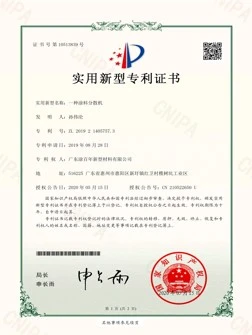
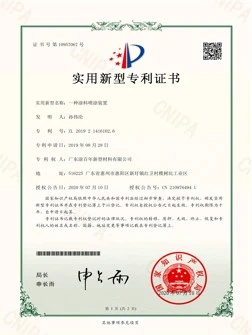
ISO Certified Quality: Strictly under ISO9001/14001 systems & 13 patents.
-
1,000,000-Ton Capacity: Engineered for major construction and bulk demands.
-
Global B2B Supply: Exported over 30,000 buckets to Southeast Asia.

Our Development Journey
-
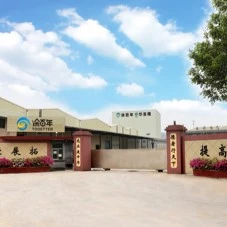 2015 | Manufacturing Foundation
Established a modern production base in Huizhou and formed strategic partnerships with major construction and real estate companies.
Expanded our eco-friendly coating portfolio and obtained multiple invention patents alongside international environmental certifications.
-
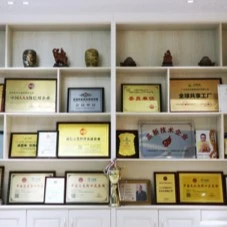 2019–2021 | High-Tech Recognition
Recognized as a High-Tech Enterprise after launching advanced eco-friendly coating solutions featuring indoor air purification technologies.
-
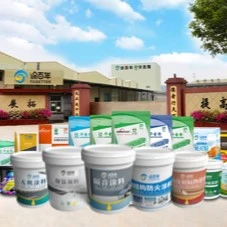 2022–2024 | Product Line Extension
Achieved the China Environmental Labeling Product Certification and developed advanced functional systems, including high-performance stone texture and thermal insulation coatings.
-
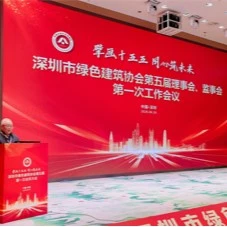 2025 | Industry Leadership & Global Reach
Recognized as a "Specialized, Refined, Unique and Innovative SME," continuously expanding cooperation with green building organizations and global partners.
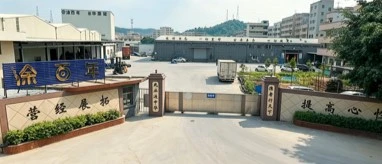
Guangdong TBN New Materials Co., Ltd. operates a modern production base in Huizhou covering over 30,000 square meters. By controlling the entire manufacturing process in-house, we eliminate middleman uncertainties and provide B2B partners with stable, efficient, and large-scale architectural coating production.
1,000,000-Ton Capacity: Built to comfortably fulfill large-scale engineering projects.
ISO Certified: Strict manufacturing management under ISO9001 & ISO14001.
Near-Zero Color Difference: Automated systems guarantee batch-to-batch consistency.
Comprehensive Output: Seamlessly producing exterior, interior, and floor coatings.
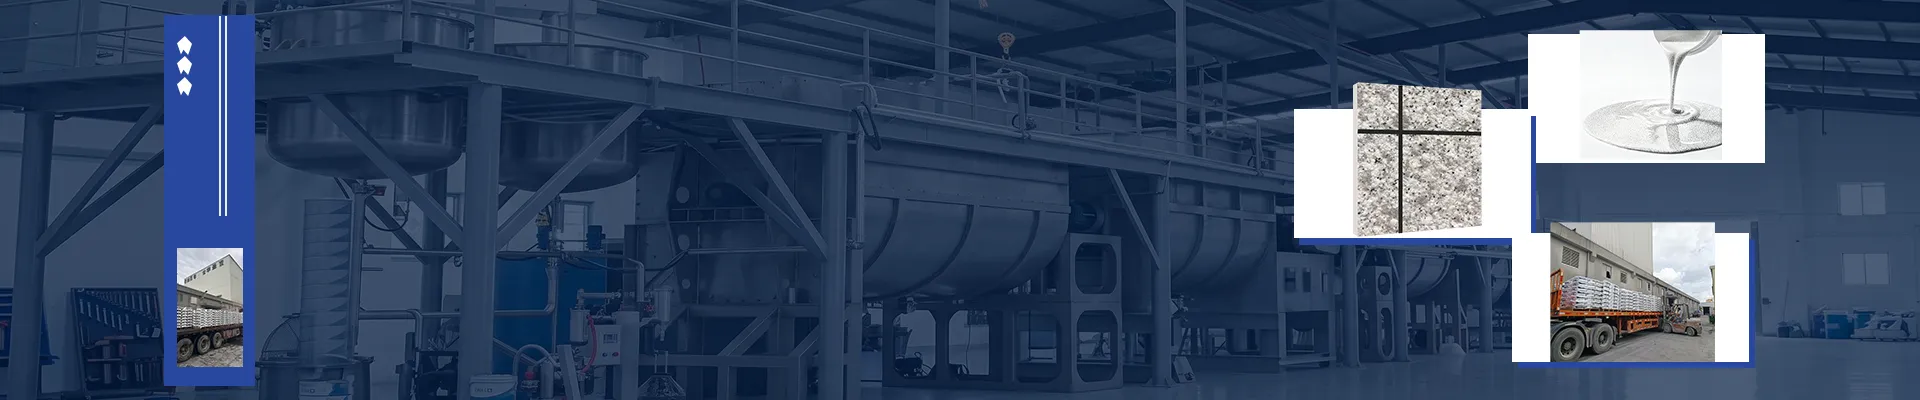
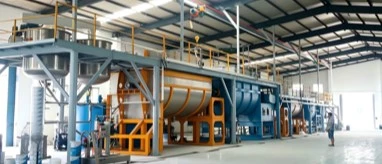
High-Speed Dispersion Mixers
Advanced mixing equipment ensures uniform formulation and premium texture for stone coatings and latex
15 Automated Production Lines
Fully automated filling and packaging lines minimize human error and support massive B2B output efficiency.
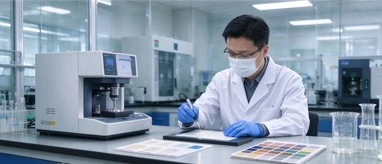
In-House QC Laboratory
Rigorous quality control inspections covering raw materials to finished products ensure compliance with global standards.
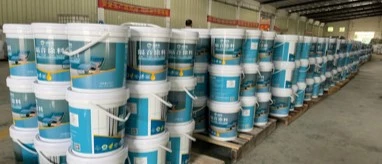
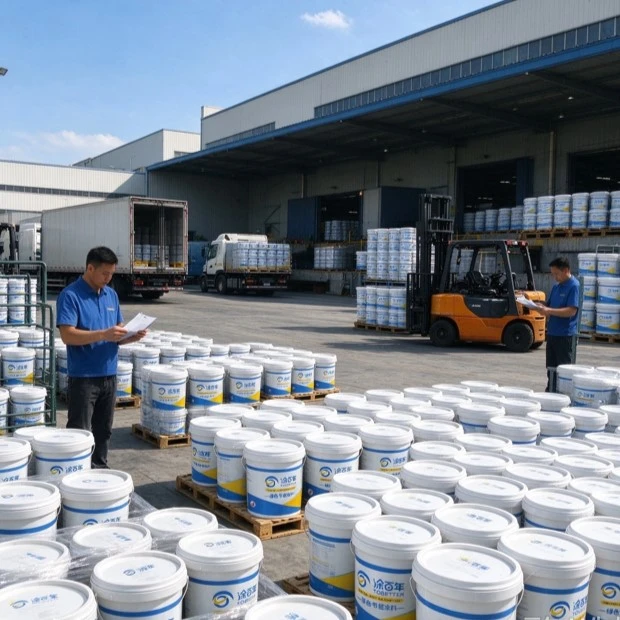
Large-Scale Warehousing
Sufficient inventory capacity and secure palletized packaging ensure stable and on-time global delivery for bulk orders.
Securing Your Supply Chain: R&D, Quality & People
TOBETTER integrates advanced formulation research, strict quality control, and a highly stable workforce to eliminate risks from your global supply chain.
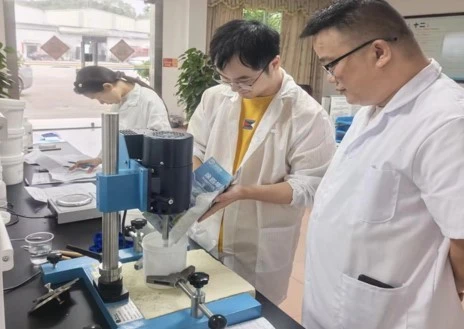
Problem-Solving R&D
Backed by 13 patents, our High-Tech R&D center engineers custom formulations. Whether you need extreme weather resistance or precise color matching, we guarantee your local market success.
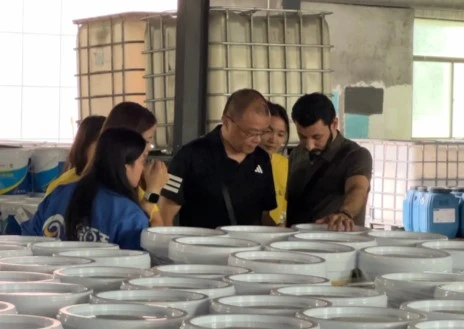
Zero-Tolerance QC
Inconsistency kills projects. Operating under ISO9001:2015, we enforce rigorous testing to ensure zero batch-to-batch color variation, preventing costly on-site rework.
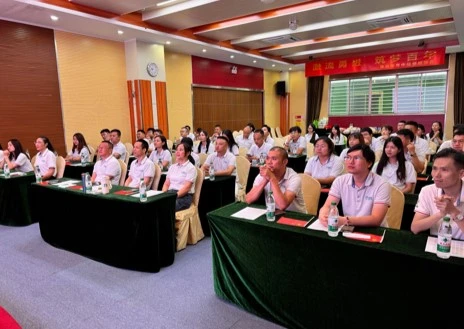
Dedicated Workforce
Through continuous professional training and weekly culture-sharing sessions, we maintain a highly cohesive workforce. Your bulk orders are consistently managed by experienced staff who understand your standards.
Global Compliance & Certifications
Backed by ISO standards, environmental labels, and 13 patents to ensure smooth customs clearance and reliable global B2B supply.